Proven Results

    Case Studies &
    Appreciation Letters

    Review measured outcomes from named installations alongside equipment details, operating context, and available appreciation letters.

    Up to 24% on Furnaces
    Up to 36% on Ovens
    12
    Documented Studies
    8–36%
    Energy Savings Range
    496+
    Tons CO₂ Reduced
    8+
    Industries Served
    Furnace Case Studies
    24%
    LPG Fuel Savings

    Lakshmi Machine Works (LMW)

    Sealed Quench Furnace — 930°C

    Textile Machinery
    Location
    Coimbatore, India
    Fuel
    Electricity & LPG
    Coating
    TCC™ 1200 (Internal) + TCC™ 400 (External)
    ROI / Payback
    4 months

    Annual savings of ₹7.54 lakhs with ROI in just 4 months

    TCC™ 1200 was applied internally on the SQF and TCC™ 400 on the external shell. Significant reduction in shell temperature and improvement in temperature gain rate per minute. Total annual cost saving of ₹7.54 lakhs with ROI in just 4 months.

    LPG Fuel Reduction
    24%
    2,300 → 1,800 Kg/month
    Electric Power Reduction
    4%
    50,000 → 48,000 kWh/month
    Set Temp Time Reduction
    12%
    34 min → 30 min
    Shell Temp Reduction
    12.5%
    70°C → 61°C
    CO₂ Reduction
    45 tons/yr
    Expected annually
    22%
    Specific Fuel Savings

    Vulkan Technologies Pvt. Ltd

    Annealing Furnace

    Forging
    Location
    Pune, India
    Fuel
    LPG
    Coating
    TCC™ 1200

    22% specific fuel reduction with 33.24 tons/yr CO₂ emission savings

    Application of TCC™ 1200 on the annealing furnace resulted in a 22% reduction in specific fuel consumption and 21% reduction in fuel consumption rate, leading to substantial fuel savings and notable reduction in carbon emissions.

    Specific Fuel Reduction
    22%
    0.13 → 0.10 kg LPG/kg material
    Fuel Rate Reduction
    21%
    14.5 → 11.34 kg/hr
    CO₂ Reduction
    33.24 tons/yr
    139.13 → 105.89 tons/annum
    22%
    Energy Savings

    Rolex Rings Pvt. Ltd

    Heat Treatment Furnace — 800°C

    Bearings & Forging
    Location
    Gujarat, India
    Fuel
    Electricity
    Coating
    TCC™ 1200 + TCC™ 400

    Heating time to 800°C reduced by 2 hours 40 minutes per batch, wall temperature down 16°C

    Even with 1,000 kg more weight in the after-coating scenario, energy consumption dropped by 437 kWh (11.43%). Adjusted for actual weight, savings amounted to approximately 12%. Heating time to 800°C was reduced by 2 hours 40 minutes per batch.

    Energy Savings
    22%
    3,822 → 3,385 kWh (11.43% with extra load)
    Heating Time Saved
    2h 40m
    12h 30m → 9h 50m
    Batch Time Saved
    7h 40m
    70h 30m → 62h 50m
    Wall Temp Reduction
    16°C
    Average surface reduction
    17%
    Power Savings

    Delphi TVS

    Sealed Quench Furnace — 930°C

    Automotive
    Location
    Sriperumbudur, Chennai
    Fuel
    Electricity
    Coating
    TCC™ 1200 (Internal) + TCC™ 400 (External)
    ROI / Payback
    4 months

    ₹4.64 lakhs/year savings with ROI in just 4 months

    TCC™ resulted in 17% power reduction and 25 minutes saved per load. Annual power savings of 46,425 units with cost savings of ₹4.64 lakhs/year. ROI achieved in just 4 months.

    Power Reduction
    17%
    869 → 720 units/day
    Process Time Saved
    25 min
    231 → 206 min per load
    Recovery Time Saved
    16%
    126 → 106 min
    CO₂ Reduction
    43 tons/yr
    Expected annually
    13%
    Specific Energy Savings

    Varroc Engineering

    Sealed Quench Furnace — 930°C

    Automotive
    Location
    Aurangabad, India
    Fuel
    Electricity
    Coating
    TCC™ 1200 (Internal) + TCC™ 400 (External)

    51 tons/annum CO₂ reduction expected over 5 years

    13% reduction in specific energy consumption with 12% faster time to achieve set temperature. Shell temperature losses reduced by 14% and temperature gain improved by 10%. Expected 51 tons/annum CO₂ reduction over 5 years.

    Specific Energy Reduction
    13%
    2.09 → 1.9 kWh/kg
    Set Temp Time Reduction
    12%
    123 → 108 min
    Temperature Gain Improvement
    10%
    1.83 → 2.04 °C/min
    CO₂ Reduction
    51 tons/yr
    Expected annually
    40–70°C
    Shell Temp Drop Savings

    Maruti Suzuki India Ltd

    Turbine Duct — 700–800°C

    Automotive
    Location
    Gurgaon, India
    Fuel
    PNG
    Coating
    TCC™ 400

    Thermal imaging verified 25–30% temperature reduction with zero coating degradation

    Demonstration of TCC™ 400 on a turbine duct operating at 700–800°C. Thermal imaging confirmed a net reduction of 40–70°C in coated areas with overall temperature reduction of 25–30%. Coating remained intact with no signs of peeling or cracking.

    Shell Temp Reduction
    40–70°C
    In coated areas
    Overall Temp Reduction
    25–30%
    Verified by thermal imaging
    Coating Integrity
    Intact
    No peeling, cracking after 10 days
    Oven Case Studies
    36%
    WDO Oven Savings

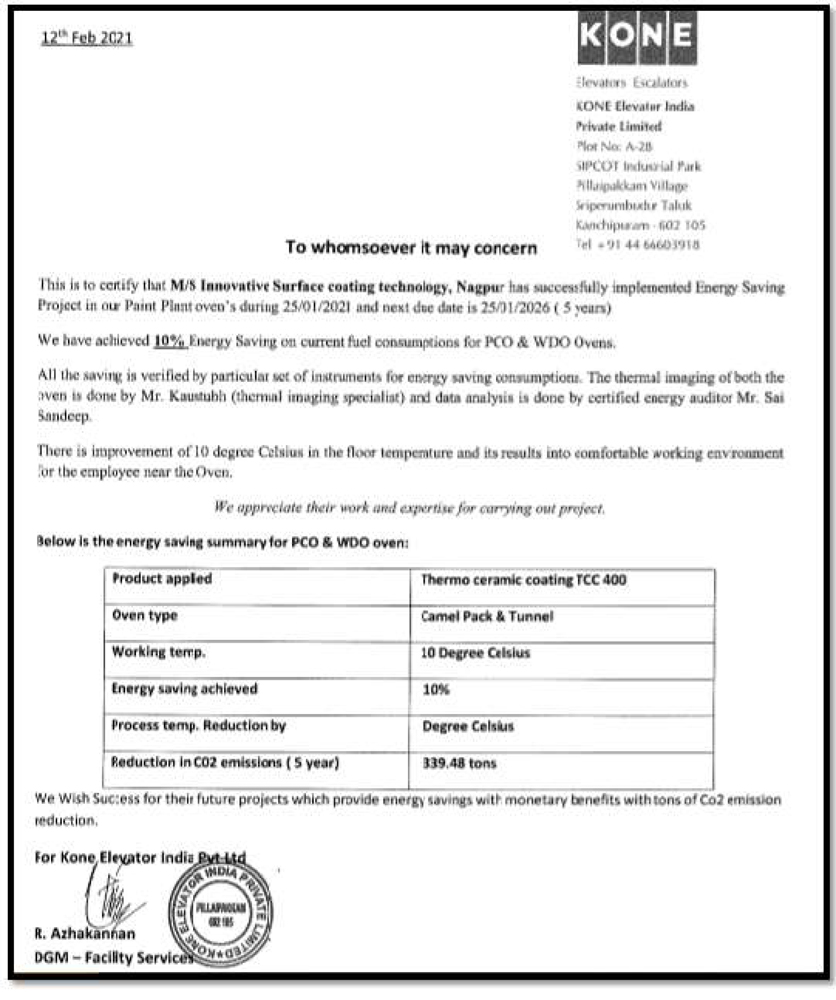
    KONE Elevator India Pvt. Ltd

    Water Dry-Off & Powder Baking Ovens

    Elevator Manufacturing
    Location
    SIPCOT, Chennai
    Fuel
    LPG
    Coating
    TCC™ 400

    36% fuel reduction in WDO oven with 18.6% overall paint shop savings

    TCC™ reduced intensity of thermal radiation between the adjacent WDO and PBO ovens. Specific fuel consumption was reduced by 36% for WDO and 11% for PBO. Overall paint shop fuel consumption reduced by 18.6%. Residence time at 180°C also reduced by 2 minutes.

    WDO Fuel Reduction
    36%
    Water Dry-Off Oven
    PBO Fuel Reduction
    11%
    Powder Baking Oven
    Overall Paint Shop Saving
    18.6%
    Combined fuel reduction
    Skin Temp Improvement
    11°C
    Oven surface temperature
    33%
    Gas Cost/kg Savings

    Pascal Switch Care

    Powder Coating Oven

    Switchgear
    Location
    Kolkata, India
    Fuel
    LPG
    Coating
    TCC™ 400

    90% heat loss reduction from oven body with 21.4% productivity increase

    The ideal heating time decreased from 27 to 16 minutes. Outside heat loss from the oven body was reduced by 90%. Conveyor speed increased from 0.70 to 0.85 m/min, leading to a 21.4% increase in productivity with 33% reduction in actual gas cost per kg.

    Gas Cost Per Kg Reduction
    33%
    Actual gas cost per kg of metal
    Productivity Increase
    21.4%
    Conveyor speed: 0.70 → 0.85 m/min
    Heating Time Reduction
    41%
    27 min → 16 min
    Heat Loss Reduction
    90%
    From oven body
    23%
    Energy Savings

    Mungi Engineering

    Conveyor Powder Coating Oven — 220°C

    Engineering
    Location
    Pune, India
    Fuel
    Gas Fired
    Coating
    TCC™ 400 (150–200 micron)

    23% energy conservation with increased production and no surface finish deterioration

    TCC™ 400 was applied at 150–200 micron thickness on the internal surface of a 1,000 sq.ft conveyor powder coating oven. The client realised 23% improvement in energy conservation with increased production without deteriorating surface finish.

    Energy Conservation
    23%
    Verified improvement
    Area Coated
    1,000 sq.ft
    Internal surface
    18%
    Power Savings

    Perkins India Pvt. Ltd

    Liquid Baking Oven — 90–100°C

    Diesel Engines
    Location
    Shendra MIDC, Aurangabad
    Fuel
    Electricity
    Coating
    TCC™ 600 (250 micron)

    31% faster heat recovery with 26% faster start-up time

    TCC™ was applied to the internal GI surface of a liquid baking oven. The client achieved 18% reduction in energy consumption, 26% faster start-up, and 31% faster heat recovery.

    Power Consumption Reduction
    18%
    18.3 → 15 L/cycle
    Start-up Time Improvement
    26%
    11.5 → 8.5 min
    Recovery Time Improvement
    31%
    8 → 5.5 min
    15%
    Fuel Savings

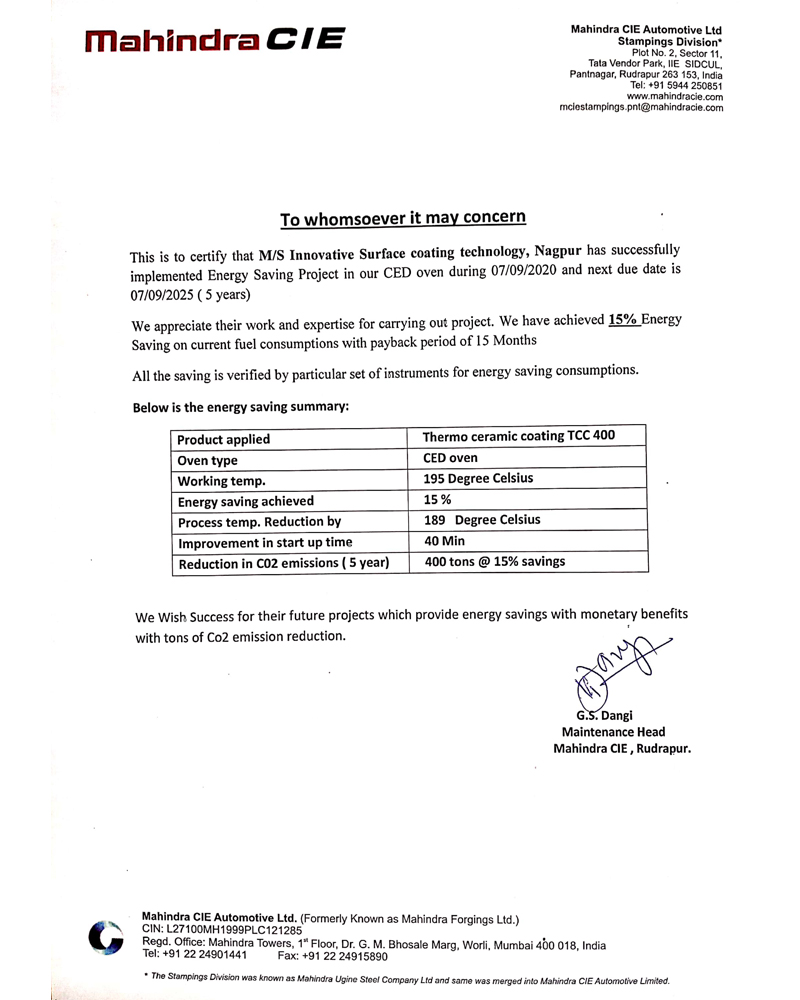
    Mahindra CIE Automotive Ltd

    CED Oven — 180°C

    Automotive
    Location
    Rudrapur, Uttarakhand
    Fuel
    Propane
    Coating
    TCC™ 400 (250 micron)
    ROI / Payback
    Under 12 months

    ₹82,000–₹1,00,000/month savings with 30 extra production minutes per day

    TCC™ applied on 4,000 sq.ft CED oven. 15% fuel saving with startup time improved by 33%. Mahindra CIE gained 30 additional production minutes per day. Monetary savings of ₹82,000–₹1,00,000 per month.

    Fuel Reduction
    15%
    12,000 → 10,200 kg/month
    Startup Time Improvement
    33%
    90 → 60 min
    CO₂ Reduction (5 yr)
    324 tons
    Verified
    Monetary Savings (5 yr)
    ₹49–60 lakhs
    ₹82K–1L/month
    10.2%
    Fuel Savings

    Hero MotoCorp

    Liquid Baking Oven

    Automotive
    Location
    Dharuhera, Haryana
    Fuel
    Gas
    Coating
    TCC™ 400

    45.3% shell temperature improvement allowed 10°C set temperature reduction

    Thermo-Ceramic Coating™ led to 22-minute reduction in startup time, 45.3% shell temperature improvement, and a 10°C reduction in required set temperature — contributing to sustained energy conservation.

    Startup Time Saved
    22 min
    90 → 68 min per cycle
    Fuel Savings
    10.63 SCM/day
    43.5 → 32.8 SCM
    Shell Temp Improvement
    45.3%
    49.3°C → 35.2°C
    Set Temp Optimized
    10°C
    150°C → 140°C
    Client Testimonials

    Appreciation Letters

    Available letters from named manufacturers provide project-specific feedback on ISCT Thermo-Ceramic Coating™.
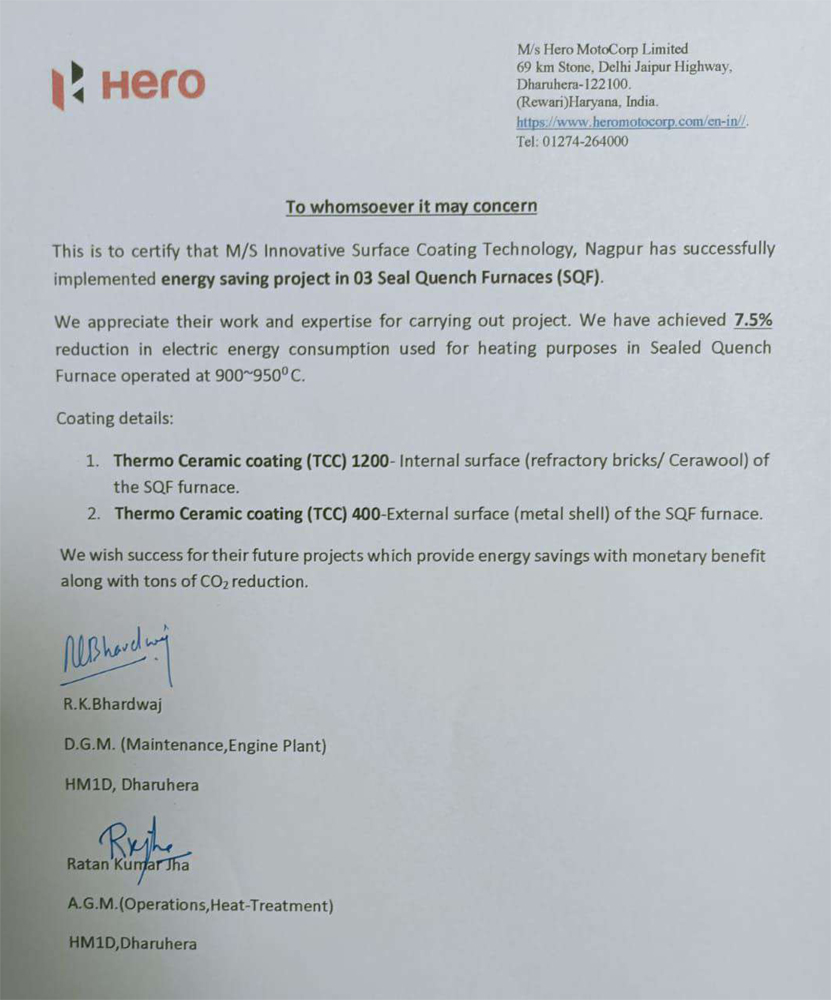
    Appreciation letter from Hero MotoCorp
    Hero MotoCorp
    Appreciation letter from Mahindra CIE Automotive
    Mahindra CIE Automotive
    Appreciation letter from KONE Elevator India
    KONE Elevator India
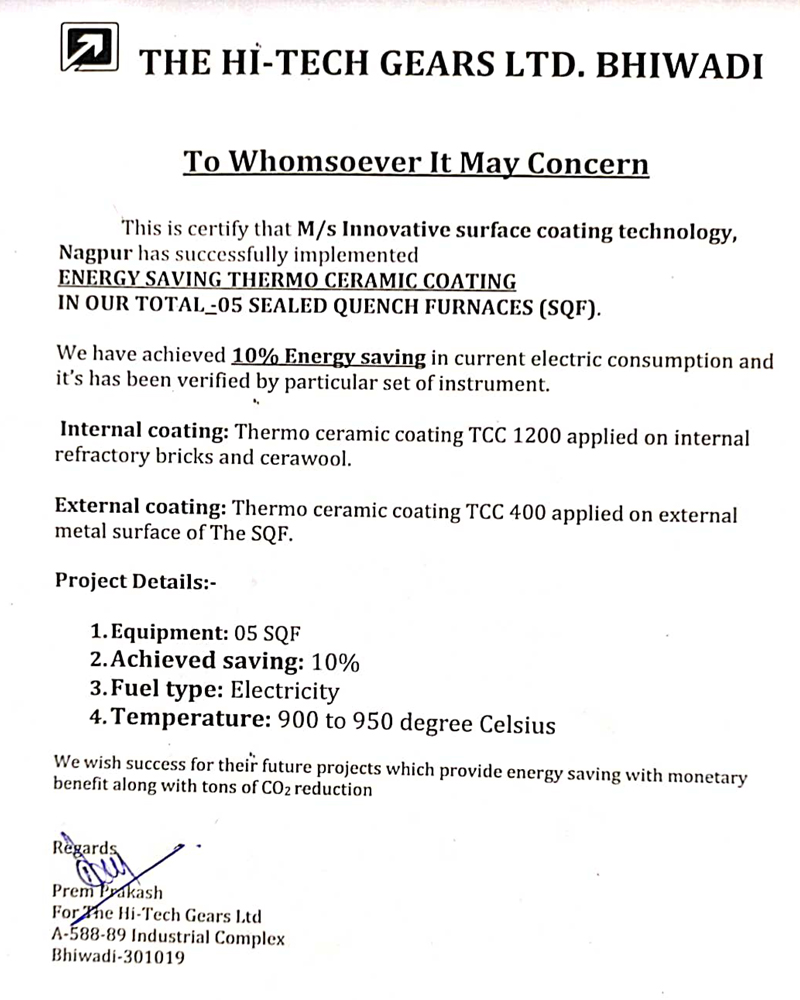
    Appreciation letter from Hi-Tech Gears Ltd
    Hi-Tech Gears Ltd
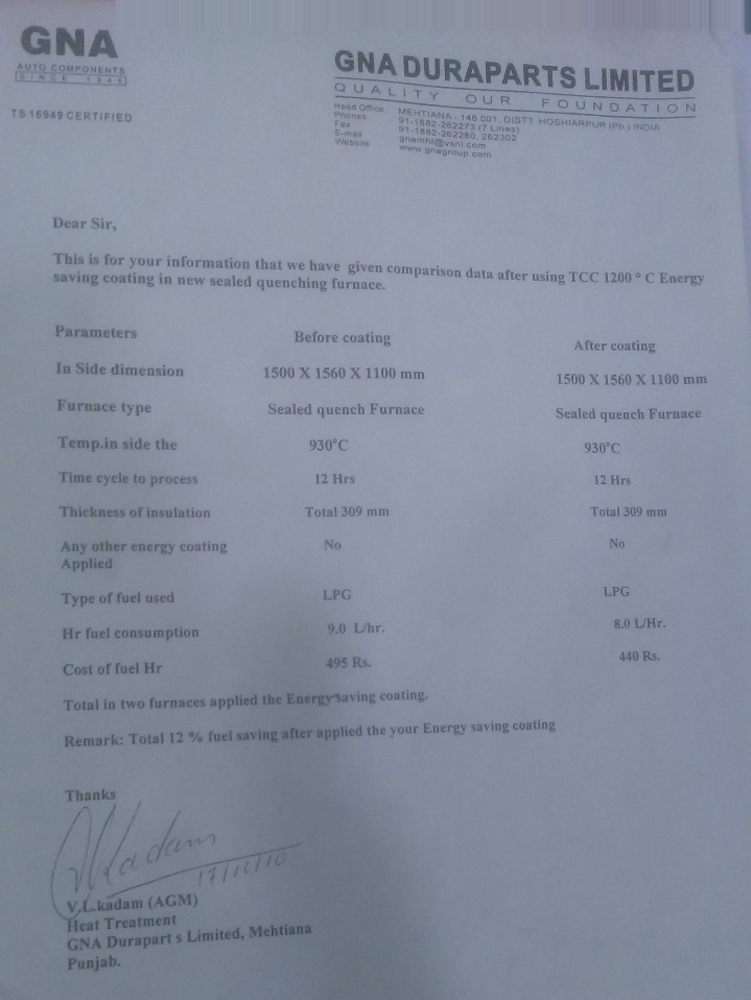
    Appreciation letter from GNA Duraparts Limited
    GNA Duraparts Limited
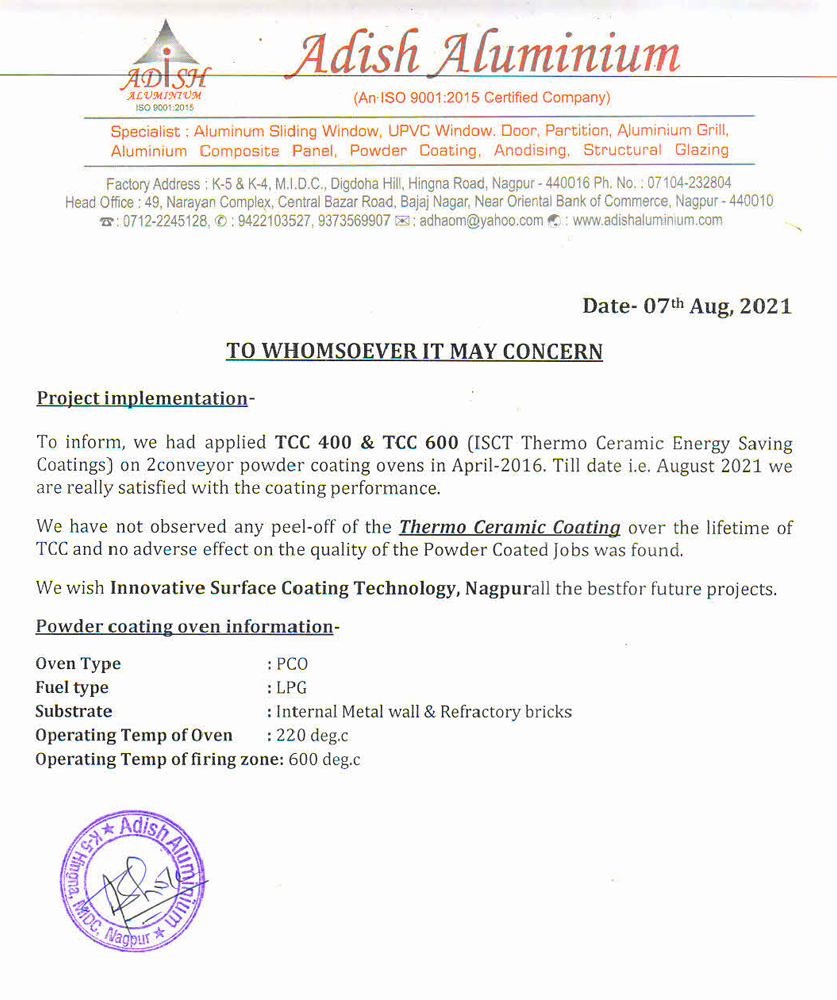
    Appreciation letter from Adish Aluminium
    Adish Aluminium
    Want Similar Results?

    Share the equipment, operating conditions, and available baseline data. The ISCT team will review the context and recommend the appropriate assessment path.